 en
 vi
 es
 th
 pt
 ms
 ko
 ru
 fr
 de
 ar
 hi
 id




Sep 18,2026
How to Choose Lens Mold Tape for Different Lens Materials
Choosing lens mold tape starts with the lens material, but material alone does not determine whether a tape will work in production. The adhesive comes into direct contact with a particular lens or mold surface, and that surface can behave differently depending on its composition, finish, coating, curvature, and manufacturing process.
A tape that performs well with one lens material may not provide the same result with another. Differences can appear as changes in holding stability, surface contact, peel behavior, or clean removal after processing. The effect becomes more noticeable when the tape remains in place during heating, curing, mechanical handling, or other demanding production steps.
For optical lens manufacturers, the useful question is therefore not simply which tape matches a particular material. It is whether the tape construction and adhesive system remain compatible with the lens material and the complete molding process.
The main material-related factors to consider are:
This is why mold tapes for optical lens applications need to be evaluated by process rather than by a single tape specification.
Resin lenses account for a wide range of optical applications, but “resin lens” does not describe one uniform adhesive environment. Different resin formulations and monomer systems can behave differently during molding and curing, which can affect how a tape performs over the entire production cycle.
During resin lens production, the tape can remain in contact with the mold assembly while the resin undergoes curing. Changes in formulation can alter the chemical environment around the tape, while changes in curing temperature or time can affect adhesive behavior.
This means a tape should not be selected solely because it has been used successfully with another resin lens. Two lenses with similar optical specifications can still require different tape performance if their resin systems or processing conditions are different.
A useful evaluation should consider:
The refractive index is still useful when identifying a resin lens and narrowing down suitable products, but it should not be treated as a complete description of the material. Refractive index does not by itself define adhesive compatibility.
The physical shape of the lens also affects tape performance. Curved surfaces require the tape to maintain consistent contact without excessive lifting, wrinkling, or local stress.
For a lens with a more demanding geometry, tape conformability becomes important. The backing needs enough flexibility to follow the surface while retaining enough mechanical strength for handling and removal.
The relevant factors include:
A tape that appears suitable on a flat test surface may behave differently when applied to a curved lens or mold. Production trials should therefore use representative geometry whenever possible.
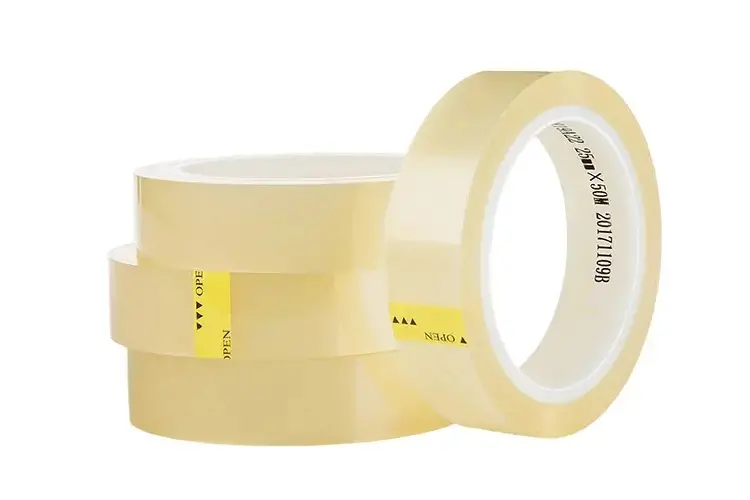
Glass lenses create a different set of considerations for lens mold tape. Compared with resin systems, the glass surface itself may have different characteristics, while polishing, coating, cleaning, or other surface treatments can further change the adhesive interface.
The objective remains the same: stable positioning during the required process without creating excessive adhesion or unwanted surface effects during removal.
A clean glass surface provides a relatively consistent substrate, but the actual surface condition still matters. Residual cleaning agents, polishing compounds, coatings, or other contaminants can change the way the adhesive contacts the surface.
This is particularly important when a production line changes its cleaning procedure. A tape that previously showed stable performance may behave differently after a change in cleaning chemistry or surface preparation.
For glass applications, qualification should therefore consider the actual surface condition rather than testing only a generic glass sample.
Glass lens production may involve handling or processing forces that make secure positioning important. If the tape does not maintain adequate contact, movement can occur during processing. Excessive adhesion, on the other hand, may make removal unnecessarily difficult.
The desired result is stable fixation with controlled release.
For production teams, this means evaluating the tape under the actual combination of:
The material category provides the starting point, but the production environment determines the final tape requirements.
The same base material can produce different tape performance when its surface condition changes. This is one of the most commonly overlooked factors in material-based tape selection.
A resin lens with a treated surface, for example, should not automatically be treated as equivalent to an untreated resin surface. The same principle applies to glass lenses with coatings or specialized surface finishes.
Three factors should be checked together:
These factors determine the actual interface that the adhesive encounters.
Surface contamination can also create misleading test results. If tape adhesion changes from one trial to another, the problem may not originate from the tape itself. Inconsistent cleaning, handling marks, or residue from previous processing can all change the contact surface.
For this reason, material compatibility testing should use production-representative surfaces and a controlled preparation procedure.
The lens material is only one part of the selection process. Processing conditions can change the requirements significantly, particularly when the tape remains in place through curing or elevated-temperature operations.
A tape may perform well during application but behave differently after prolonged exposure to heat. Likewise, a tape that removes cleanly immediately after processing may show different peel behavior after cooling or after remaining on the mold for an extended period.
| Production condition | Tape property to evaluate | Typical concern |
|---|---|---|
| Curved lens or mold surface | Conformability | Edge lifting or incomplete contact |
| Mechanical handling | Holding stability | Movement or displacement |
| Elevated temperature | Thermal stability | Adhesive softening or transfer |
| Long contact time | Adhesive stability | Increasing peel force |
| Repeated handling | Backing strength | Stretching or tearing |
| Post-process removal | Release behavior | Residue or difficult peeling |
The complete thermal and mechanical history matters. Maximum temperature is useful information, but it does not tell the whole story. A production cycle with a moderate temperature held for a long period can place different demands on an adhesive from a short exposure to a higher temperature.
This is also why lens mold tape should be tested under conditions that reproduce the real manufacturing cycle whenever practical.
Material-based selection becomes more useful when it is connected to the actual production requirement rather than treated as a simple material-to-tape chart.
For conventional resin applications, the tape generally needs a balanced combination of:
The resin formulation and curing conditions should be supplied to the tape manufacturer during qualification. If the production process uses a specific monomer system or a particularly long curing cycle, those details can be more useful than simply identifying the lens as “resin.”
High-index resin lenses deserve additional attention because the resin system, lens geometry, and processing conditions may create tighter performance requirements. However, the refractive index itself should not be used as the only selection criterion.
For a deeper discussion of the material and process factors involved, high index lens mold tape can be evaluated in relation to the specific resin and molding conditions.
The key point is that high-index applications should be assessed as a combination of material chemistry, geometry, curing conditions, and tape performance.
For glass applications, the main considerations are surface compatibility, secure positioning, and controlled removal.
Particular attention should be given to surface coatings and cleaning procedures. A tape that works on untreated glass should not automatically be approved for coated or specially treated glass without testing.
Where the tape is used for positioning rather than long-term protection, the removal process also needs to be considered from the beginning. Easy removal is useful only if the tape remains stable throughout the required production stage.
Tape data sheets can narrow down suitable options, but they cannot replace application testing. The most reliable evaluation uses the actual lens material, representative mold surface, and production process.
The tape should remain securely positioned during the intended process. Testing should look beyond initial tack and consider whether the bond remains stable after temperature exposure and mechanical handling.
A useful test should record whether:
After removing the tape, inspect both the tape and the surface.
Look for:
The inspection should be performed consistently so that small differences between tape samples can be identified.
Clean removal should be evaluated after the complete production cycle, not only immediately after tape application.
A practical qualification sequence is:
Repeated testing matters because one clean peel does not establish production consistency.
A material category is a useful starting point, but it does not contain enough information to define the complete tape specification.
Consider two resin lens production lines using the same basic resin type. One may use a different curing temperature, another may have a different mold surface, and a third may require longer tape contact. The tape requirements can therefore change even though the nominal lens material remains the same.
A more reliable selection sequence is:
Lens material → surface condition → lens geometry → processing conditions → tape construction → production validation
This approach also prevents a common purchasing mistake: selecting tape based on one specification while overlooking the conditions that actually determine performance.
For example, a tape with strong adhesion may appear attractive from a product data sheet, but stronger adhesion is not automatically better. If the production process requires clean removal after curing, excessive adhesion may increase peel force or create adhesive transfer.
Likewise, a highly flexible tape may conform well to a curved surface but still be unsuitable if its backing cannot withstand the required handling.
The goal is a balanced tape system that matches the complete application.
Standard products are often sufficient when the material, mold geometry, and production conditions fall within established application ranges. Customization becomes more useful when a defined production requirement cannot be addressed reliably with a standard construction.
Typical reasons to consider customization include:
Customization should begin with a specific production requirement rather than a general request for “stronger” or “higher-temperature” tape.
The manufacturer may need information about the lens material, mold surface, processing temperature, contact time, application method, and removal process before recommending changes to the backing or adhesive system.
Before approving a tape for production, the purchasing and engineering teams should be able to answer the following questions:
| Selection question | Why it matters |
|---|---|
| What is the lens material? | Establishes the basic application environment |
| Is the surface coated or treated? | Changes adhesive interaction |
| What is the lens or mold geometry? | Determines conformability requirements |
| What temperatures will the tape experience? | Defines thermal stability requirements |
| How long will the tape remain in place? | Affects adhesive stability |
| How will the tape be removed? | Determines release requirements |
| What level of residue is acceptable? | Defines surface cleanliness requirements |
| Is the process manual or automated? | Influences backing and roll specifications |
The most reliable lens mold tape is not necessarily the one with the highest adhesion, the thickest backing, or the strongest temperature rating. It is the tape that maintains the required positioning and surface contact for the entire production stage while remaining compatible with the material and allowing controlled removal afterward.
For optical lens manufacturers, material compatibility, surface condition, process stability, and removal performance should be evaluated as one system. That approach gives the tape selection process a much stronger technical basis and reduces the risk of discovering compatibility problems only after production has started.